SmartWire-DT wiring system in plastics production facility
Upgrade provides individual drive motor power measurement and real-time operator visualisation to reduce production line downtime.
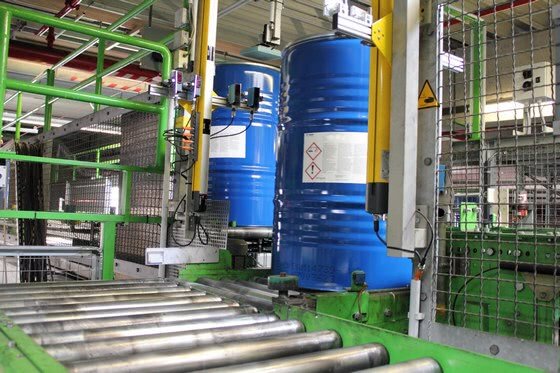
BASF Polyurethanes GmbH is based in Lemförde near Osnabrück, Germany, and at this facility the 1,500+ staff generates sales in excess of two billion Euros. The barrel conveyor system is a key part of the plant. It transports 200-litre barrels with finished products and raw materials from two production halls to the barrel storage area or from the warehouse to production.
Throughout the facility, no buffer stock is kept at individual processing stations. In the event of the transportation system stopping due to a jammed barrel or malfunction, the output of the production process can be impacted.
BASF realised that the control systems of 25-year old transportation system was outdated, and needed to be revised to meet modern manufacturing requirements.
The original plant control system
The system was controlled by three old PLCs (programmable logic controllers) that could not be supported, as spare parts were no-longer manufactured. The safety levels were not state-of-the-art and BASF had no plant visualisation. No manual correction action could be taken prior to a failure.
The decision was taken to improve both the automation process and enhance the safety technology. A further stipulation was that the 50 three-phase motors driving the transportation system had to remain operational during the upgrade.
The solution
A central PLC was employed to autonomously control the barrel transportation system. This simplified the automation architecture and the consolidation into one control cabinet freed up valuable space on the production floor. At critical points in the system, operator panels were installed to aid visualisation. Operators could identify barrels that were not been removed from the transport mechanism in real-time, and easily see where congestion was occurring.
The panels are also able to provide information for preventative maintenance as the system displays the type of error occurring. The ability to distinguish if a run-time error is due to a drive overcurrent event or a frequent start-stop condition for example, provides valuable information to the maintenance teams. Proactive action can now be taken to test the drives or preform an inspection of the mechanical system.
To enable error detection, the BASF team paid close attention to measuring the current drawn by the drive motors. “This was the main reason for us to wire the control cabinet with Eaton’s SmartWire-DT intelligent wiring system,” explains Thomas Büch, a member of Site Engineering Lemförde’s Technical Team.
The switchgear and drives are not connected with individual point-to-point wiring with the control panel; instead SmartWire-DT uses an eight-pole flat cable. The one cable supplies all the devices with power and simultaneously takes care of the data communication.
“By using system tools and components, wiring errors are virtually eliminated,” explains Thomas Gern, Head of the Industrial Systems Technology department at Elektro-Anlagen-Technik EAT GmbH. Based in Wallenhorst, Germany, the electro-technical service provider built the control cabinets for the BASF plant. “Routine testing of the cabinet can therefore take place within a very short time. After a brief system introduction at our end, our control cabinet makers were able to complete wiring in half the time in comparison with conventional point-to-point wiring.”

Increasing plant up-time and improving safety
The use of Eaton PKE motor-protective circuit-breakers allowed expanded drive monitoring. Diagnostic, status and overload messages show the actual flow of current and the status of the trip device. This information is displayed and analysed via the SmartWire-DT system without the need for additional components.
By operating the PKE as a motor protection relay rather than a breaker, in the event of a jammed barrel on the transportation system the relay will open until the obstruction is removed. The control panel can then be used to switch the motor back on, rather than having to wait for an electrician to restart production. This not only reduces downtime, but enables the PKE device to be mounted in locations that are not readily accessible.
Previously, if an emergency button was activated, the entire transportation system stopped. Restart was only possible from a central location. Now, individual safety zones have been created by using power-feed modules to supply power to the switchgear using SmartWire-DT. In the event of an emergency stop, only the relevant power-feed module and the high-level redundant group contactor to that particular zone are switched off. Authorisation to re-start is available from the operator control panel.
Conclusion
Using Eaton technology, BASF has reduced downtime in their barrel transportation system. SmartWire-DT simplified the upgrade, and the use of individual drive current measurement has allowed faults to be localised and rectified faster. Implementing motor protection relays in place of breakers enables an overload condition to be remedied, with motor reset via a control panel. This avoids the need for maintenance personnel having to first reset a protection switch, and hence production is quickly restarted. It also reduces the need to call in electricians during the night and at weekends.

Source: Eaton
Read more: